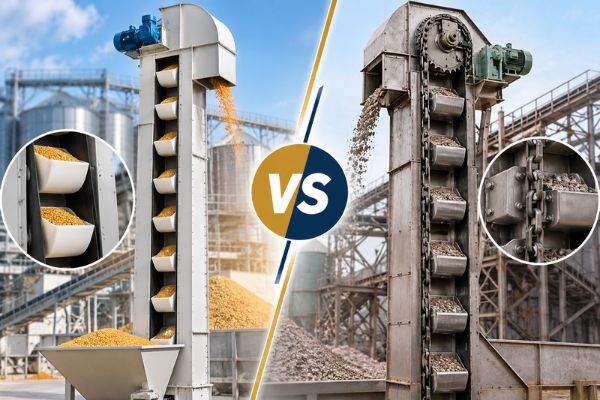
Belt vs Chain Bucket Elevator Which Is Right for Your Industrial Plant

Which Bucket Elevator Fits Your Material and Operating Conditions A belt bucket elevator is often suitable for bulk materials within the selected belt’s temperature and loading limits. A chain bucket elevator can be considered for hotter or demanding material duties. The correct choice depends on the complete operating conditions, including particle size, abrasiveness, capacity and…
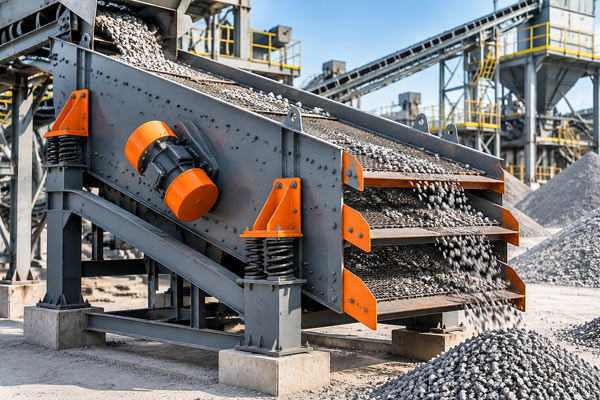
Industrial Vibratory Screen Manufacturer for Efficient Screening

Industrial Vibratory Screen Manufacturer for Efficient Screening Efficient material separation is an important part of bulk material handling. Industries dealing with powders, granules, minerals, chemicals, food ingredients, ash, coal and other bulk materials need consistent screening to maintain product quality and protect downstream equipment. This is where an Industrial Vibratory Screen Manufacturer plays an important…

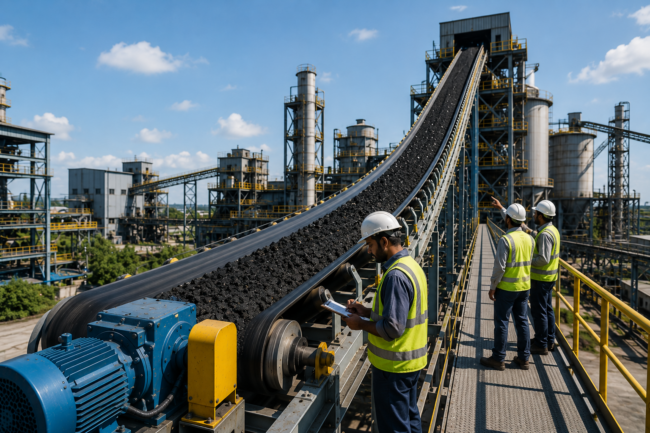
Smart Industrial Belt Conveyors for Energy Efficient Material Handling

Smart Industrial Belt Conveyors for Energy Efficient Material Handling Industrial plants are under growing pressure to move more material while using less energy, reducing downtime and maintaining safer working conditions. Because of this, belt conveyors are changing from simple transport equipment into smarter material handling systems that support efficient plant operations. For cement plants, steel…

Material Handling Equipment Manufacturer in India

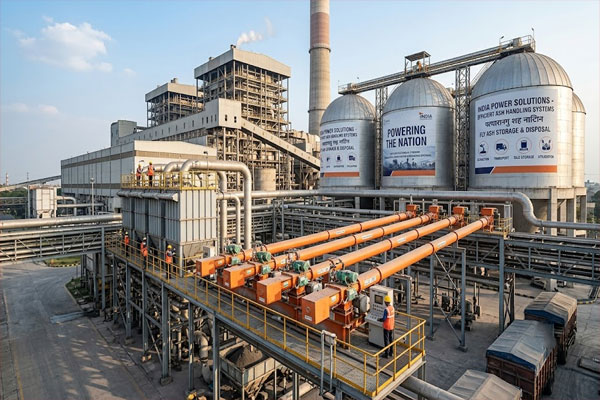
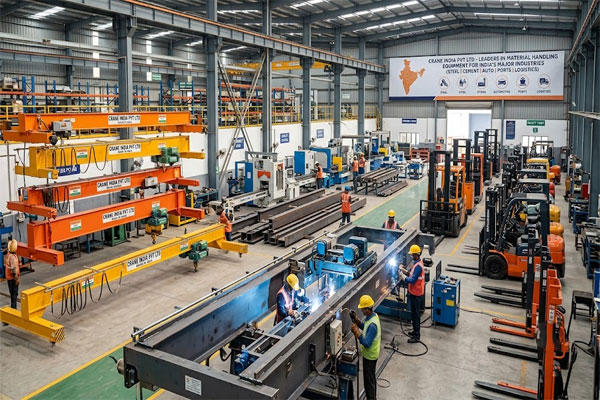
Material Handling Equipment Manufacturer in India for Major Industries

Material Handling Equipment Manufacturer in India for Major Industries Efficient material movement is essential for the smooth operation of modern industrial plants. Industries need reliable systems to transport, lift, feed, store and process raw materials safely. Cement, steel, power, mining, chemical, food, pharmaceutical and infrastructure plants depend on specialized equipment to maintain continuous production. Choosing…